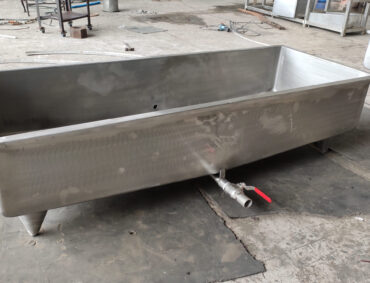
Fabricated with heavy-gauge AISI SS 304/316 food-grade stainless steel, engineered for 24/7 continuous hygienic operation, high thermal efficiency, and minimal dairy maintenance.
Heat Recovery Units Tanks (HRUs) are devices used to recover waste heat generated from various industrial processes or systems. They typically consist of heat exchangers designed to capture and transfer thermal energy that would otherwise be lost. Here are brief descriptions of common types of HRUs:
These units transfer heat between two air streams, typically exhaust air and incoming fresh air. They are common in HVAC systems to improve energy efficiency by preheating or precooling incoming air using the exhaust air.
These units transfer heat between two water streams. They are used in industrial processes where hot water from one process can be used to heat another process or to preheat water entering a boiler or other equipment.
HRSGs recover heat from gas turbine exhaust to generate steam. This steam can be used for various purposes, including power generation or industrial processes requiring steam.
These units recover heat from exhaust gases produced by engines or industrial processes. The recovered heat can be used for heating water, space heating, or for other industrial applications.
Uses : Food oil tanks are used to store a variety of cooking oils, such as vegetable oil, olive oil, canola oil, and others used in food preparation. They help in keeping oils fresh and free from contaminants.
Although not strictly HRUs, plate heat exchangers are often used in heat recovery applications due to their efficiency in transferring heat between two fluids separated by plates.
Each type of HRU is designed based on the specific application requirements, such as temperature range, flow rates, and the nature of the fluids involved. They play a crucial role in improving energy efficiency and reducing operating costs in various industries.
Authoritative technical answers regarding capacity sizing, food-grade sanitary construction, Clean-In-Place (CIP) cleaning, and dairy plant integration from Aviva Equipments engineers.
Heat Recovery Units Tanks capture the high-grade waste superheat discharged by refrigeration compressors and bulk milk coolers. Instead of venting heat into the atmosphere, the HRU transfers this energy into incoming cold water, generating free hot water up to 60°C–65°C.
The recovered hot water is immediately piped for pre-heating boiler feedwater, crate and can washing docks, or initial CIP (Clean-In-Place) pre-rinse cycles, saving substantial diesel, gas, or electrical boiler heating expenses.
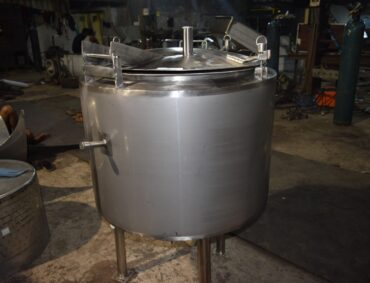
Aviva Equipments manufactures heat recovery tanks in capacities from 500 Litres to 10,000 Litres, engineered with internal food-grade SS 304/SS 316 heat exchanger coils that withstand high refrigerant discharge pressures.
Because dairy refrigeration units run continuously during daily milk intake, Aviva HRU tanks typically pay for themselves within 6 to 14 months purely through fossil fuel and electrical energy savings.
As respected dairy plant machinery manufacturers, Aviva provides integrated thermal engineering that harmonizes refrigeration pressure drops with heat exchange thermodynamics, guaranteeing optimal compressor lifespan and thermal efficiency.
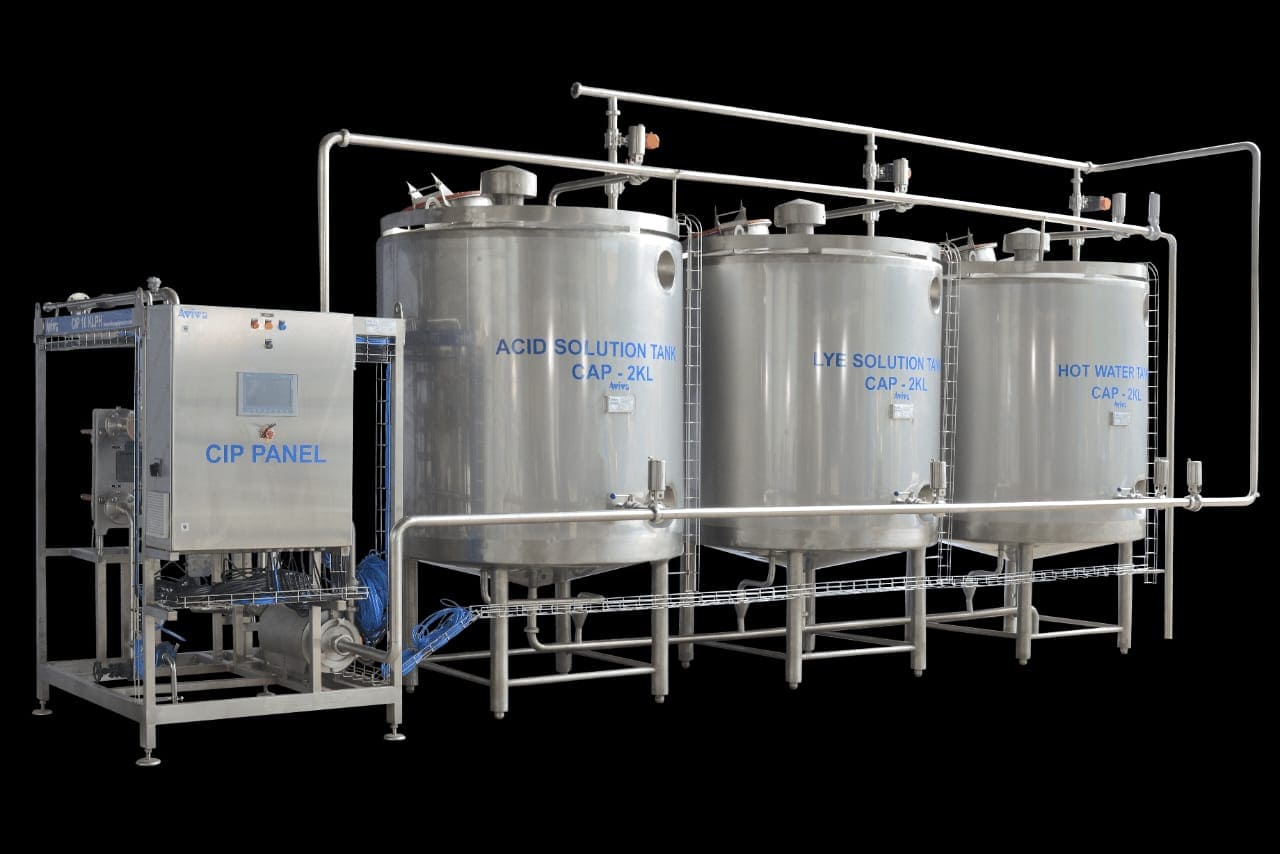
Consult with Aviva Equipments engineering team for custom capacity sizing, P&ID layout drawings, and factory-direct pricing tailored to your plant.