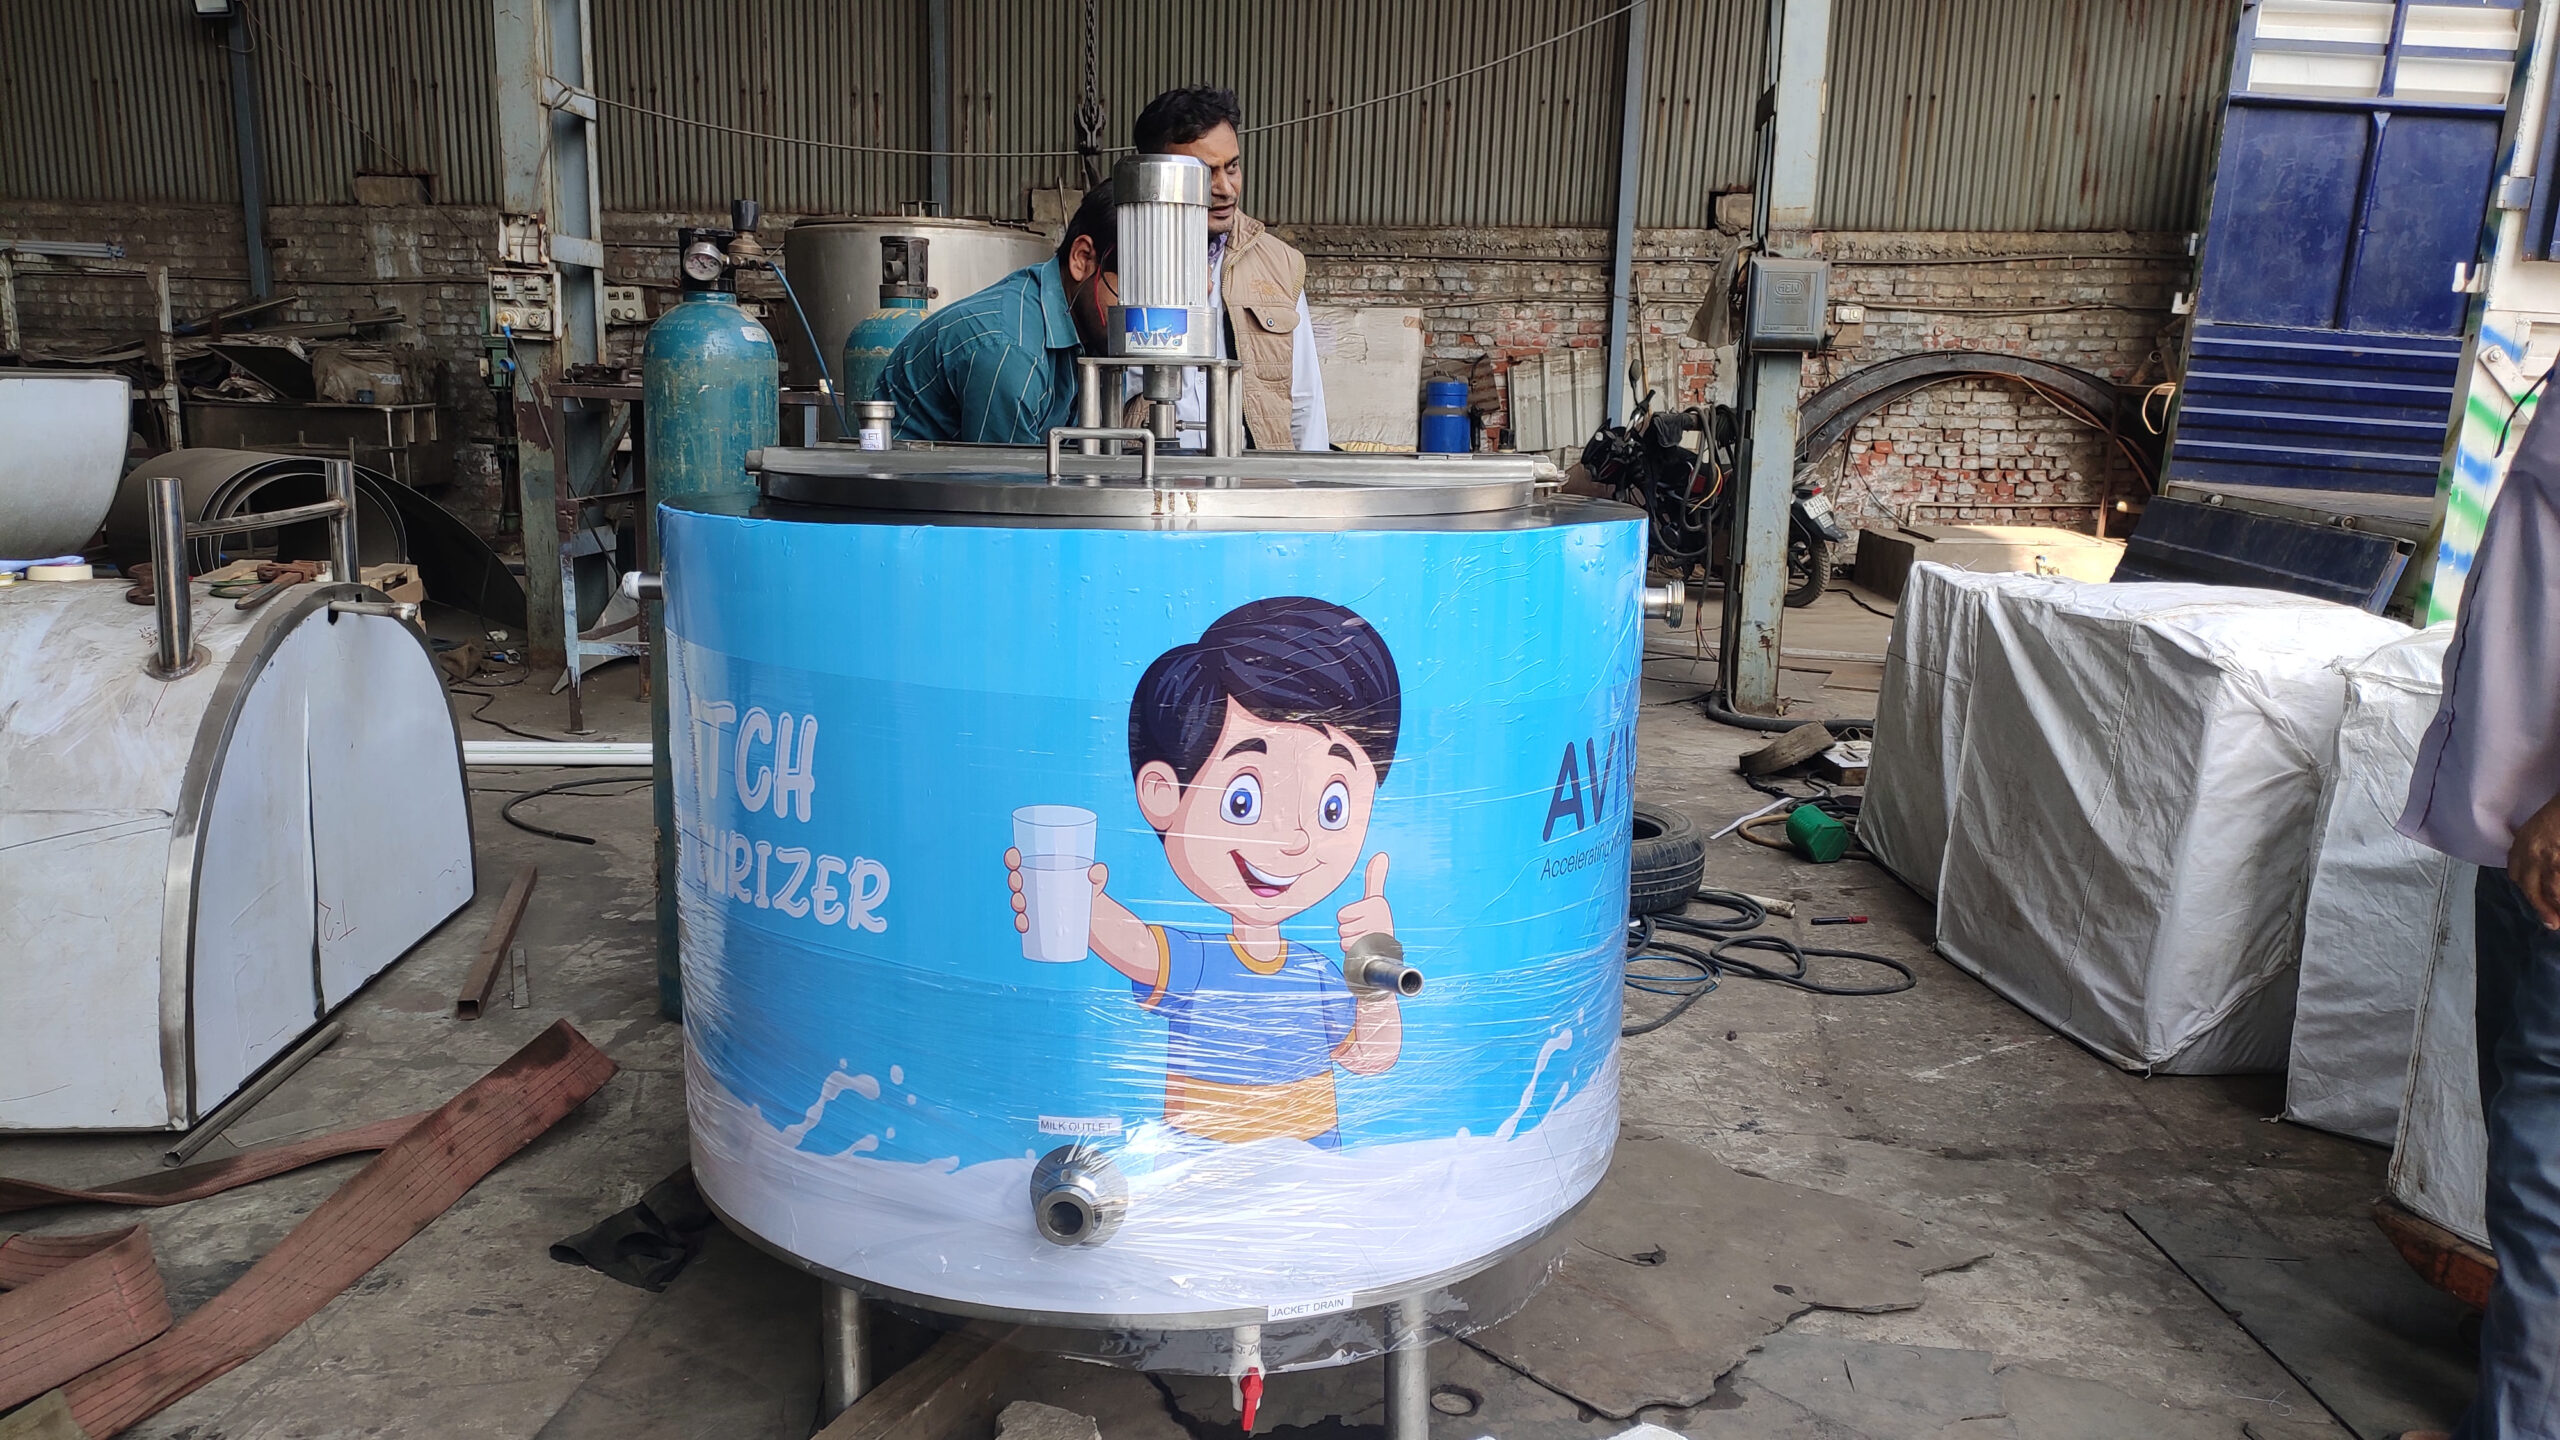
Fabricated with heavy-gauge AISI SS 304/316 food-grade stainless steel, engineered for 24/7 continuous hygienic operation, high thermal efficiency, and minimal dairy maintenance.
A ghee boiler is a specialized vessel used in the production of ghee, a clarified butter commonly used in South Asian cuisine. Here’s a general description of a ghee boiler:
Design : Typically, a ghee boiler is a large, cylindrical vessel with a capacity ranging from small-scale to industrial sizes, depending on production needs.
Function : The primary function of a ghee boiler is to melt butter and clarify it through a heating process. This involves heating the butter until it melts completely and then allowing it to simmer. During simmering, the milk solids separate and settle at the bottom, while the clarified butter (ghee) rises to the top.
Usage : Ghee boilers are used in commercial kitchens, food processing industries, and traditional ghee-making setups to produce ghee efficiently and hygienically.
| Heating Mechanism | It may have a heating element or be designed to be heated indirectly through steam or hot water circulation. |
| Stirring Mechanism | Some boilers have mechanisms for stirring to ensure uniform heating and prevent burning. |
| Temperature Control | Precise temperature control is important to ensure that the butter is heated to the right temperature without scorching. |
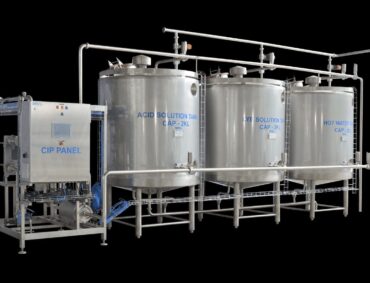
| Sanitization | Optional step using a sanitizing agent to kill microorganisms |
| Final rinse | Purified water or a final rinse solution is used to ensure all cleaning agents are removed. |
Overall, a ghee boiler plays a crucial role in the production process of ghee, ensuring that the clarified butter is produced consistently and at scale.
Authoritative technical answers regarding capacity sizing, food-grade sanitary construction, Clean-In-Place (CIP) cleaning, and dairy plant integration from Aviva Equipments engineers.
As a specialized ghee plant manufacturer, Aviva supplies complete turnkey production lines comprising butter melting vats, steam-jacketed ghee boilers/kettles, settling tanks, ghee clarifiers/separators, micro-filters, storage tanks, and automated pouch/tin filling machinery.
We engineer ghee plants in capacities from 200 Litres Per Hour (LPH) for boutique dairy farms up to 5,000+ LPH for large commercial dairy cooperatives, configured with manual, semi-automatic, or fully automated PLC controls.
Our ghee boiling kettles feature hemispherical bottoms with dimple steam jackets and variable-speed Teflon-tipped scrapers. Precise temperature control allows optimal caramelization of milk solids, creating authentic traditional aroma and golden granular ('danedar') texture.
All product contact equipment is fabricated from certified AISI SS 304 and SS 316 stainless steel with mirror-polished internal surfaces to resist free fatty acid corrosion and ensure effortless CIP cleaning.
Operating across the dairy products manufacturing machinery sector, Aviva provides comprehensive plant layout design, steam and utility piping, on-site commissioning, and recipe process optimization.
Consult with Aviva Equipments engineering team for custom capacity sizing, P&ID layout drawings, and factory-direct pricing tailored to your plant.