Fabricated with heavy-gauge AISI SS 304/316 food-grade stainless steel, engineered for 24/7 continuous hygienic operation, high thermal efficiency, and minimal dairy maintenance.
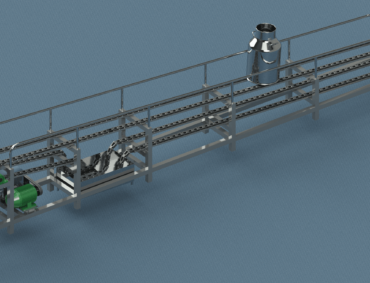
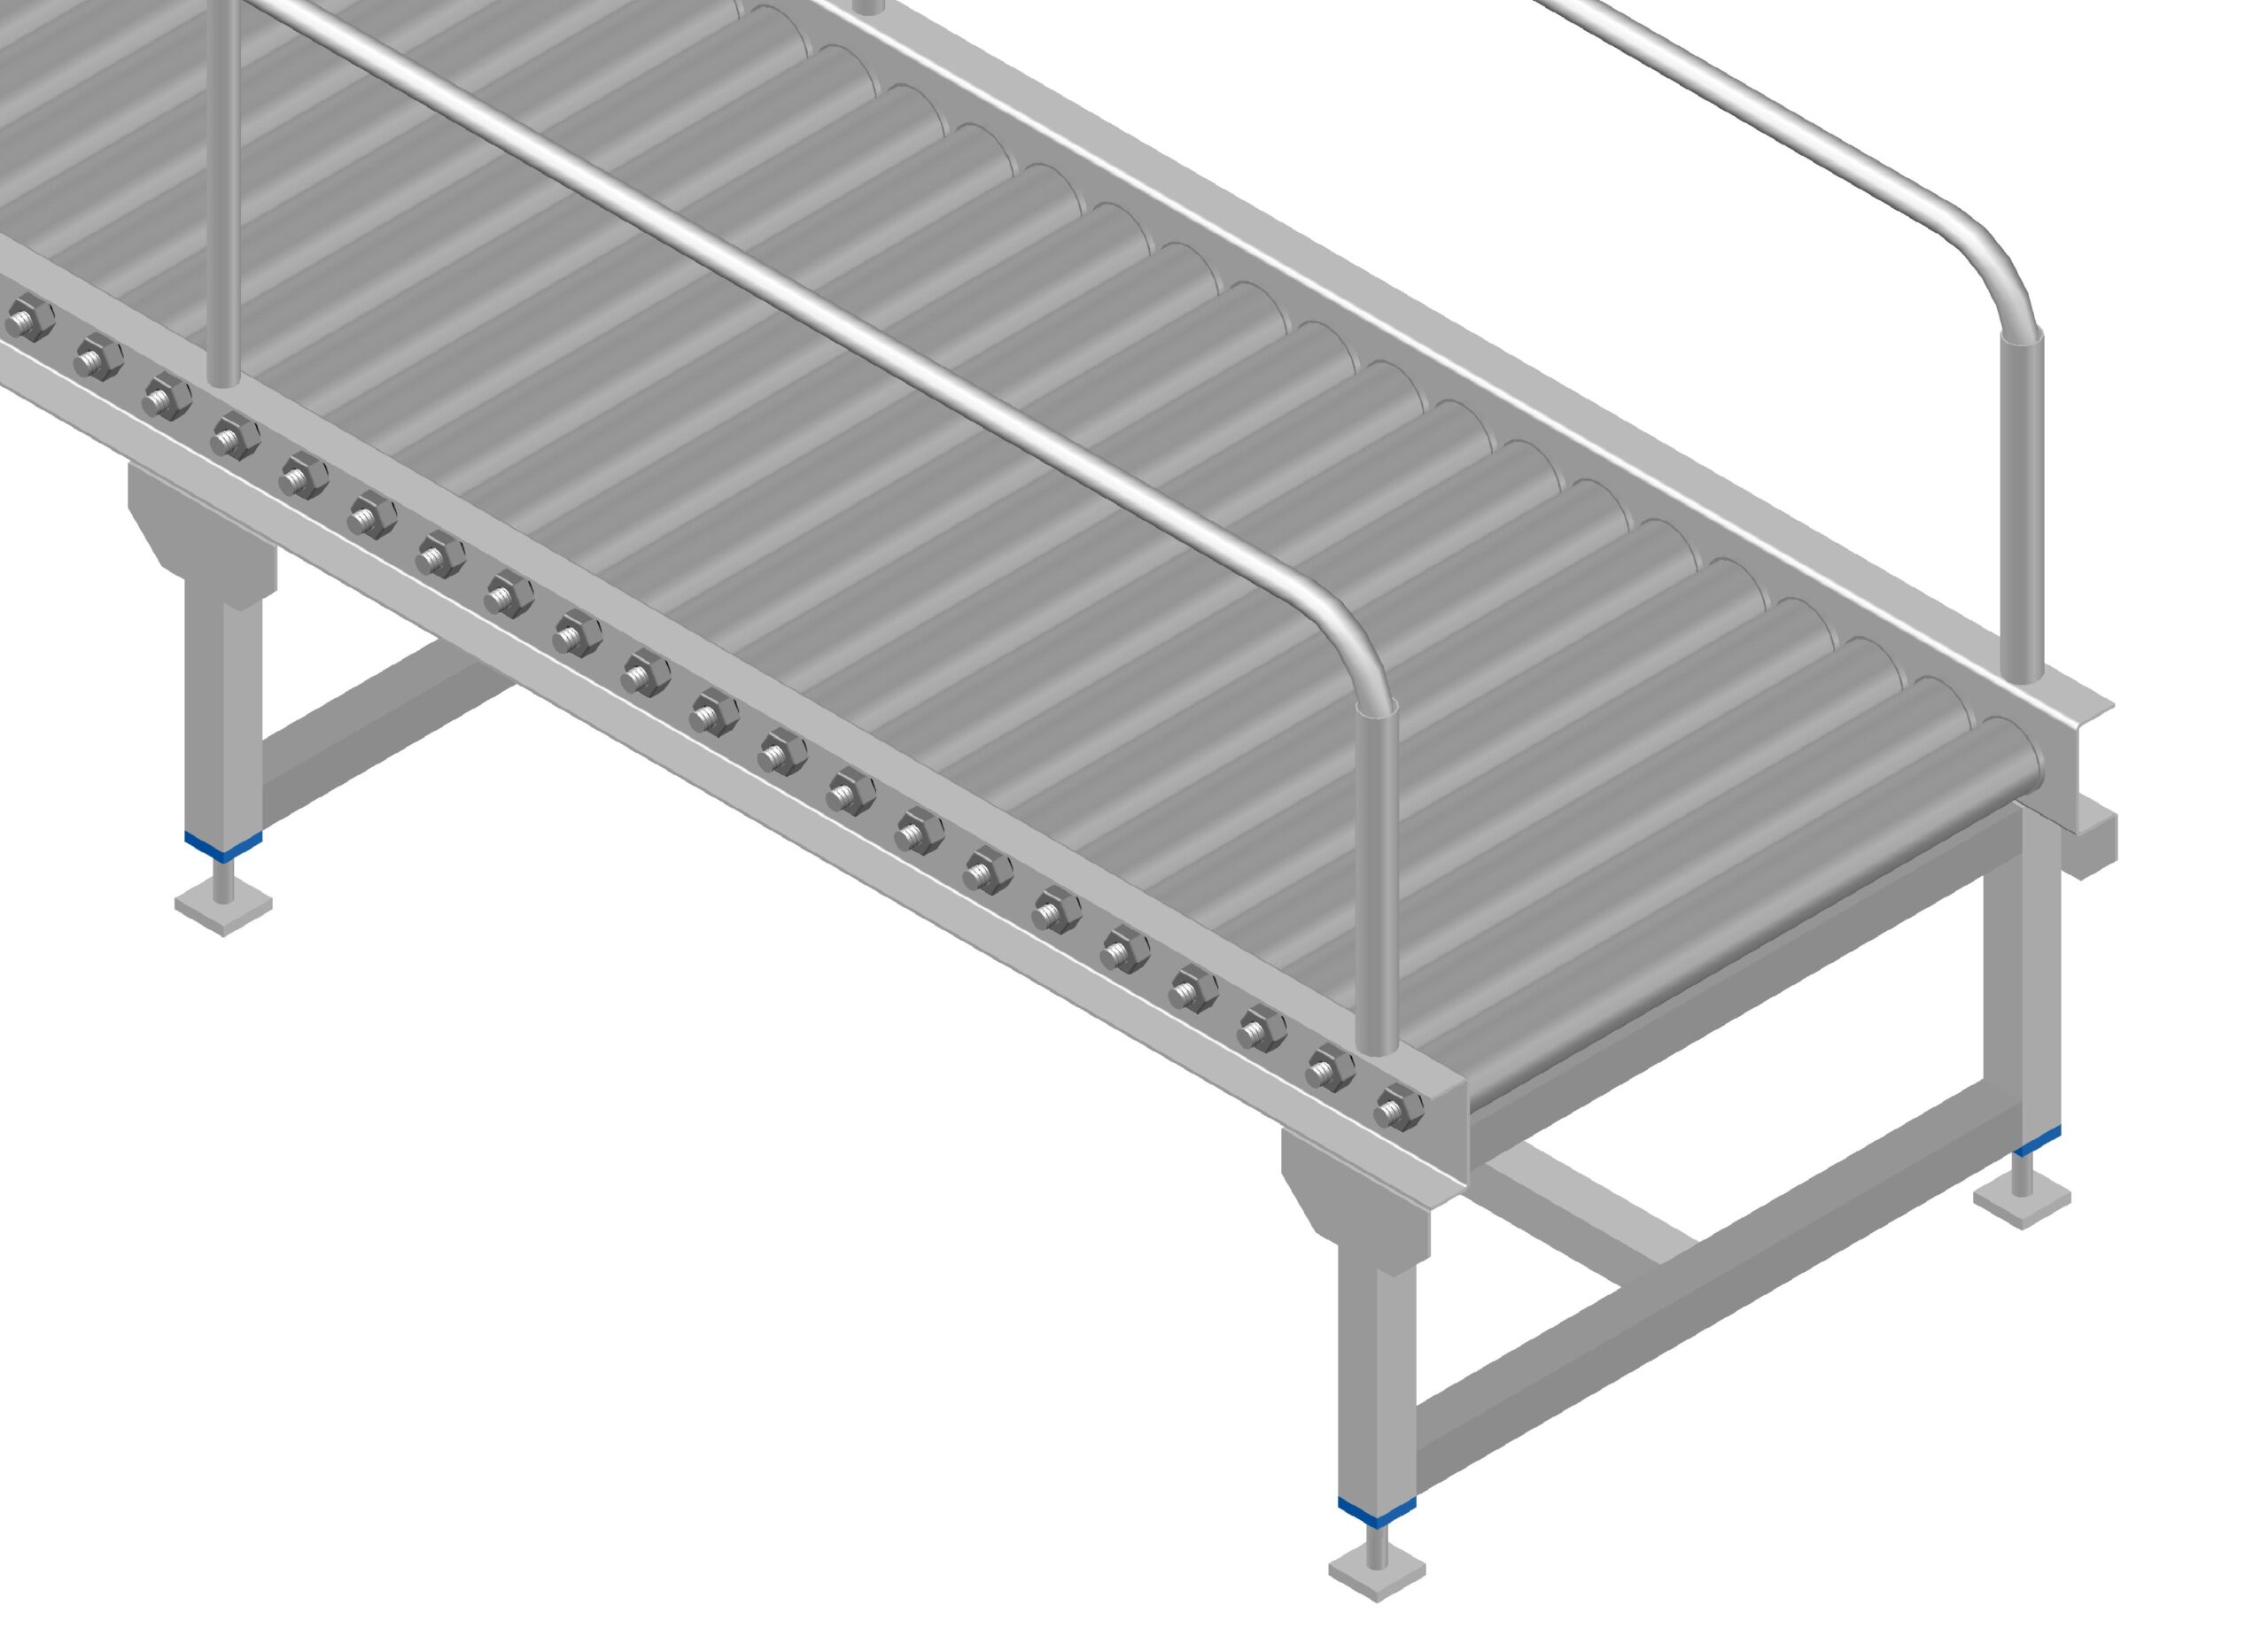
A Milk Can Conveyor is a specialized equipment used in dairy processing to transport milk cans efficiently. It streamlines the movement of milk cans within a dairy facility, enhancing productivity and automation.Milk Can Conveyors play a crucial role in optimizing the dairy production line, ensuring efficient handling and movement of milk cans. AEPLalso a manufacture of Various types of Conveyors for Food industry like BeltConveyor,Gravity Roller, Screw and Chain Conveyors in Stainless Steel. Whether you need a standard conveyor or a customized conveying systemAEPLcan Design for Your needs.
| Conveyor Type | Straight & Available in Curve Shape Also. |
| Capacity | Conveyor can Carry Filled Milk Cans up to 50 kg/feet |
| Automation Grade | Semi Automation. |
| Usage/Application | Milk Can Feeding Conveyor |
| Weight | Depends on the Conveyor Length. |
| Customization | The company offers customization options for their Conveyor to meet the Different Plants Layout |
| Gear Motor | Gear Box With 3 Hp with Standard Make |
| Gravity Roller Table | A Small Roller Table Also Attached with Conveyor. |
| Push Buttons | Start - Green Stop- Red Emergency Push Button- Provided |
| Electrical Information | Main Power – 3 X 415vac, 50hz Control Voltage- 230v Ac |
| Tipping Bar | A Tic Wood or Nylon Tip Bar Attached with Conveyor to Easily Dump Milk Cans into Weigh Bowl. |
Authoritative technical answers regarding capacity sizing, food-grade sanitary construction, Clean-In-Place (CIP) cleaning, and dairy plant integration from Aviva Equipments engineers.
A motorized chain conveyor for milk cans automates the continuous horizontal movement of heavy 40L milk cans from reception truck bays, through the weighing station, can washer, and back to loading docks, eliminating manual pushing.
Aviva utilizes specialized bi-planar or cardan stainless steel / acetal conveyor chains gliding on ultra-high-molecular-weight (UHMWPE) wear strips, delivering smooth, whisper-quiet operation and zero metal-on-metal friction.
Conveyors are powered by IP55 washdown-duty geared motors (1.5 kW to 4 kW) equipped with variable frequency drives (VFD) that allow dock operators to calibrate can speed between 500 and 1,500 cans per hour.
Our open stainless steel tubular frame prevents milk debris, curd, and water accumulation, allowing operators to pressure-wash the entire conveyor track in minutes.
As reputable dairy equipment manufacturers in india, Aviva designs custom modular straight tracks, 90-degree curves, and inclined sections tailored to your dairy reception dock floor plan.
Consult with Aviva Equipments engineering team for custom capacity sizing, P&ID layout drawings, and factory-direct pricing tailored to your plant.